
Engineered with precision, built on two decades of trust.
Evaron Pharmaceuticals began with a simple mandate: manufacture medicines with the exact precision, integrity, and safety we’d expect for our own families. Today, that principle guides every batch record we sign off across our formulation, API, and veterinary divisions.
Purpose-driven pharmaceutical manufacturing.
Every batch we process is backed by documented procedures, strict atmospheric cleanroom controls, and a commitment to global public health.
Our Mission
To manufacture safe, highly effective, and globally accessible medicines through validated processes, GLP quality control, and zero-compromise batch integrity for healthcare brands and patients alike.
Our Vision
To be the premier contract manufacturing and active ingredient synthesis partner of choice for leading human healthcare and animal health brands across India and 40+ export markets by 2030.
Our Values
Uncompromising integrity in raw material sourcing and batch documentation, continuous discipline in cleanroom protocols, and profound respect for every regulator, partner, and end-patient.
From a focused formulation line to an integrated pharmaceutical group.
Evaron was founded with one oral dosage production line and a dedicated team of pharmacists. Today, the group operates state-of-the-art facilities across human formulations, veterinary medicines, and chemical API synthesis.
We remain privately held and leadership-managed. That independence ensures that decisions regarding quality standards, capital investment, and compliance are driven by scientific necessity and personal accountability — never short-term compromises.
-
100% In-house quality control testing with analytical GLP certification.
-
Dedicated HVAC environmental zoning preventing cross-contamination.
-
Complete eCTD dossier and Drug Master File (DMF) regulatory support.

Two decades of steady milestone achievements.
Our evolution reflects structured investments in technology, classified cleanrooms, GLP analytical laboratories, and global regulatory dossiers.
First Formulation Facility
Began operations with a focused oral solid dosage production line supplying leading domestic healthcare brands under strict WHO-GMP protocols.
Veterinary Division Established
Expanded operations with a dedicated veterinary healthcare unit offering oral bolus, liquid suspensions, and feed supplements for animal health.
WHO-GMP & ISO Accredited
Comprehensive facility upgrades securing official WHO-GMP certification alongside ISO 9001:2015 and ISO 14001:2015 environmental standards.
API Chemical Synthesis Plant Commissioned
Achieved backward integration into active pharmaceutical ingredient manufacturing with specialized glass-lined reactors, micronisation bays, and DMF dossier support.
Global Supply Across 20+ Export Countries
Operating an integrated multi-facility complex with in-house R&D labs, accelerated stability chambers, and an active international regulatory affairs desk.
Facilities engineered around strict compliance.
Explore our classified cleanroom suites, analytical GLP laboratories, automated packaging bays, and chemical synthesis reactors.


Zero-defect commitment across all operations.
Click below to explore how our quality assurance protocols ensure 100% compliance with USP, BP, and IP pharmacopoeias.
Pharmacopoeial Validation
Multi-stage testing of raw materials, intermediates, and final formulations.
Integrated Infrastructure
Cleanrooms, GLP labs, and API units integrated into a 350,000 sq.ft facility.
Regulatory Dossier Readiness
Audit-ready CTD/eCTD dossier dossiers and DMF files prepared for global health authorities.
Scalable Batch Capacity
Flexible batch sizes for pilot stability runs up to multi-million commercial runs.
Zero Defect Quality Control
All active raw ingredients and finished dosage forms undergo rigorous assay, dissolution, related substances, and microbial limit testing before Certificate of Analysis release.

Unified Manufacturing Infrastructure
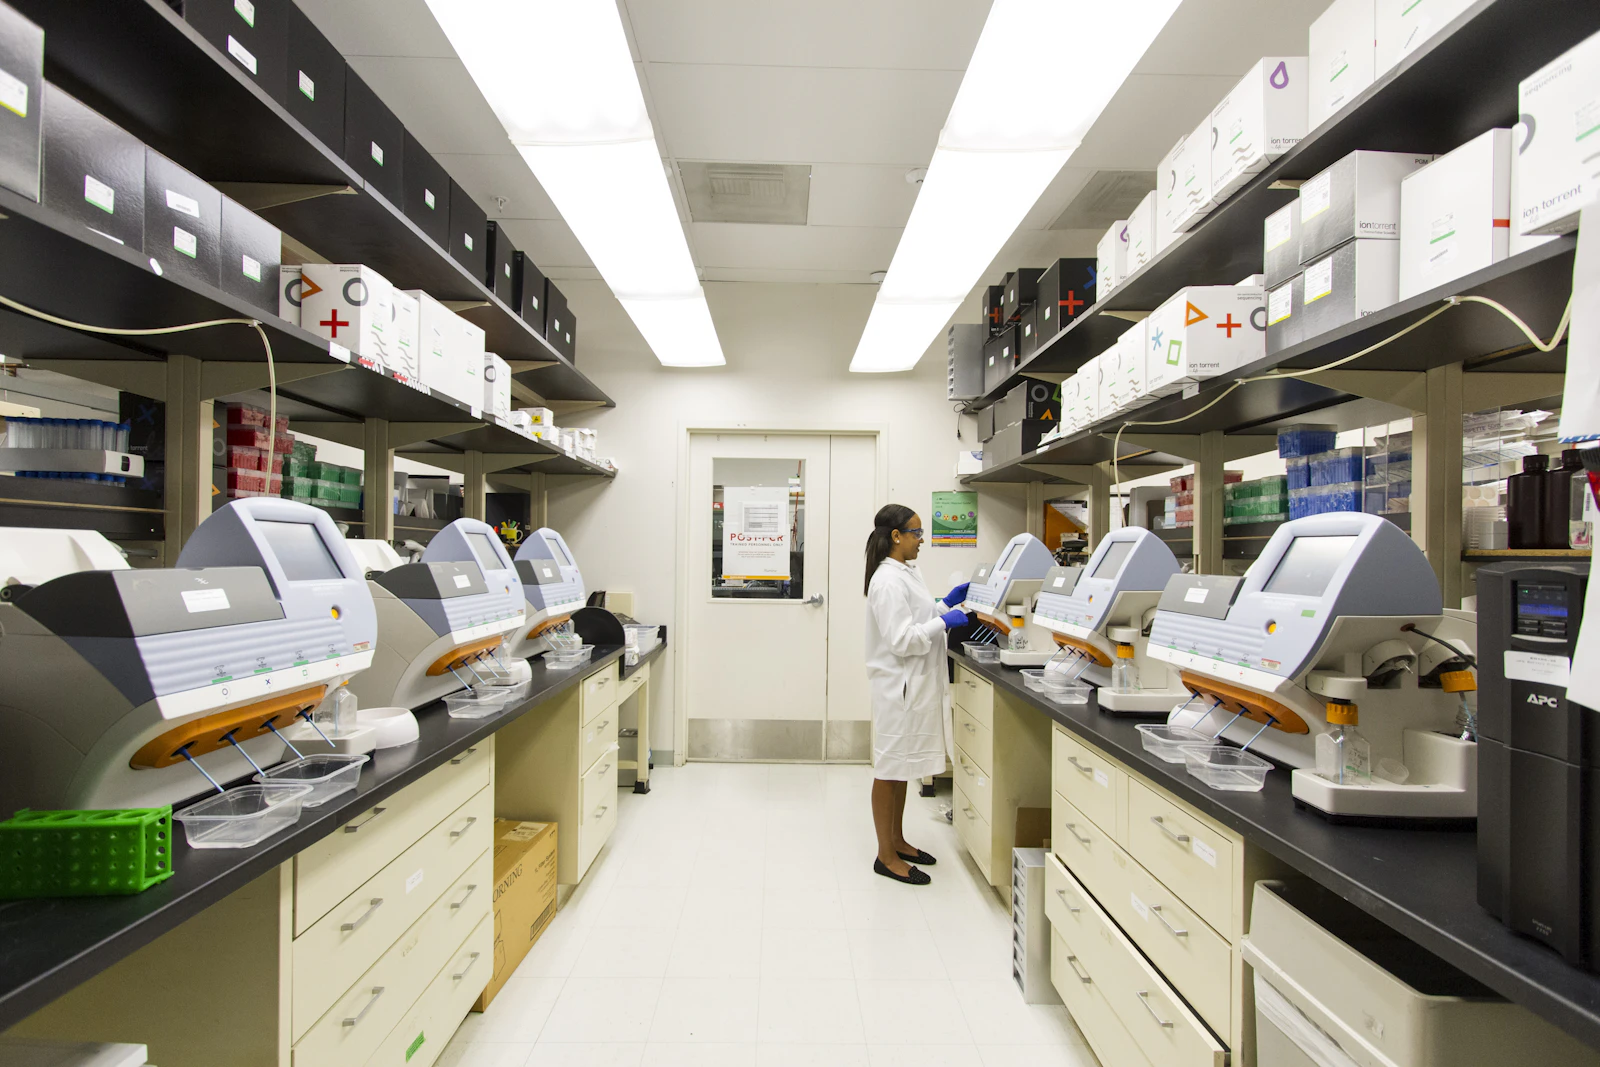
Cleanroom formulation suites, chemical synthesis reactors, GLP analytical laboratories, and temperature-controlled storage operate in one integrated, ISO-certified site.

Global Regulatory Dossier Support
Our regulatory affairs desk prepares comprehensive CTD/eCTD dossier modules, stability data packages, and DMF documentation ready for health authority audits across global markets.

Agile Scale from Pilot to Commercial
Flexible batch sizing enables pilot scale validation batches for R&D trials as well as multi-million unit commercial market supply runs on schedule.
Want to verify our quality accreditations?
Explore our complete list of WHO-GMP licenses, state FDA approvals, and ISO management certifications.