
Three specialized divisions. One compliant manufacturing network.
Evaron's production infrastructure is structured around three specialized divisions — Human Formulations, Veterinary Medicines, and Active Pharmaceutical Ingredients — all operating under a shared WHO-GMP quality management system.
Production Infrastructure
WHO-GMP AuditedPurpose-built divisions for global healthcare.
Each division operates specialized equipment, isolated handling areas, and dedicated technical teams.
 DIVISION 01
Human Formulations
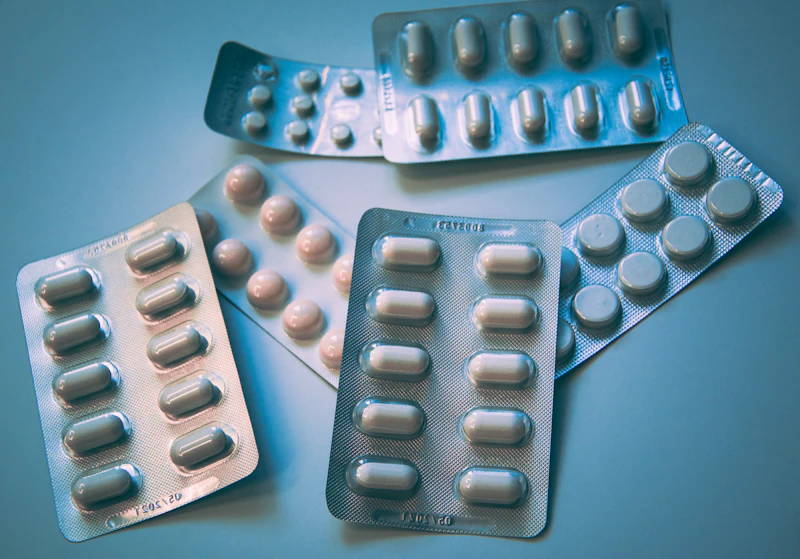
High-capacity lines for tablets, hard gelatin capsules, oral liquids, dry syrups, sterile injectables, and topical ointments.
 DIVISION 02
Veterinary Range
Feed supplements, large boluses, oral drenches, powders, and veterinary injectables for livestock, poultry, and pets.
 DIVISION 03
API & Bulk Drugs
Active pharmaceutical ingredients manufactured under stringent process controls with complete DMF dossier support.
Every division certified. Every batch documented.
Regardless of division, every product manufactured at Evaron passes through the same validated quality management system — from raw material qualification to finished-product release.
-
WHO-GMP certified cleanrooms & HVAC air-handling systems
-
ISO 9001:2015 & ISO 14001:2015 accredited operational standards
-
GLP-certified analytical testing & HPLC/GC quality control labs
-
State & Central FDA licensed manufacturing operations

From raw molecule to market in six validated stages.
Every commercial batch undergoes strict stage-gate approvals before dispatch.
R&D & Tech Transfer
Pre-formulation studies, analytical method development, and pilot scale-up.
Sourcing & Raw Material QC
Vendor auditing, incoming raw material sampling, and active ingredient assaying.
Validated Manufacturing
Environmentally controlled cleanroom processing under automated parameters.
In-Process & Final QC
Uniformity, dissolution, microbial limit, and assay verification in GLP labs.
Packaging & Serialization
Blister, Alu-Alu, bottle, and ampoule packing with 2D barcode tracking.
QA Release & Logistics
Batch record sign-off, Certificate of Analysis issuance, and temperature-monitored dispatch.

Have a formulation requirement to discuss?
Send us your product specification and target volumes — our technical team will respond within 24 hours.